Reducing Lighting-Related Maintenance Risk in Regulated Manufacturing Environments
In most buildings, a failed light fixture is an inconvenience. In a validated pharmaceutical suite, a food-contact processing room, or a Class I, Division 2 solvent-handling area, it is something else entirely: an unplanned intervention in a controlled space, a work order that has to be documented, and — depending on where the fixture sits — a potential deviation.
That distinction is the reason lighting deserves more engineering attention in regulated manufacturing than it usually receives. The purchase decision is often made on wattage, lumen output, and unit price. The consequences are felt years later by the maintenance and quality organizations, who inherit whatever access constraints, sealing limitations, and documentation gaps were baked into the original specification.
This article looks at where lighting-related maintenance risk actually accumulates in regulated environments, and what specifiers can do at design time to keep it low.
Why a Relamp Is Never Just a Relamp
Start by counting the true cost of a single luminaire failure in a controlled space. It rarely stops at parts and labor.
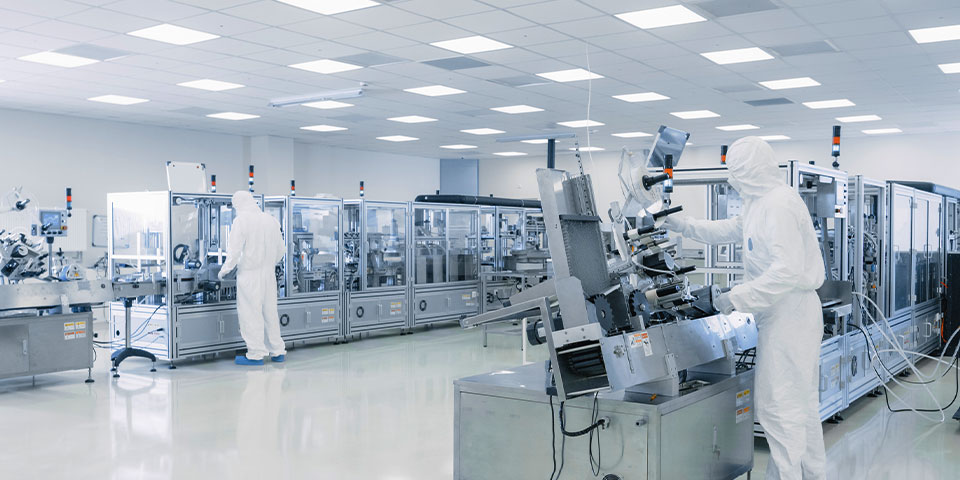
A technician entering a cleanroom or aseptic area requires gowning, and gowning requires procedure. Ladders, lifts, and hand tools introduce particulate and must be cleaned in and cleaned out. Work over open product, exposed equipment, or a filling line typically means the line stops. Depending on the classification of the space and the nature of the intervention, the room may require cleaning, re-sanitization, or environmental monitoring before production resumes. If the fixture sits in a classified electrical area, any field modification touches the listing that made the installation compliant in the first place.
Regulatory expectations reinforce this. FDA current good manufacturing practice requires that manufacturing areas have adequate lighting, which means illumination is a qualified condition, not a comfort item — and a fixture out of service in an inspection or visual-check area is a condition worth documenting. Cleanroom classification under ISO 14644 is a function of particle counts that maintenance activity directly disturbs. In classified areas, NFPA 70 governs what may be installed and how, and OSHA’s general electrical requirements require that equipment be used in accordance with its listing and labeling.
Put together, the arithmetic is straightforward. A fixture that costs a few hundred dollars can generate an intervention costing several thousand — and a quality record that outlives the fixture.
Where the Risk Actually Comes From
Across controlled-environment projects, lighting-related maintenance risk tends to concentrate in five places.
- Access was never designed. The fixture was selected before anyone asked how it would be serviced. Recessed troffers sit above a sealed ceiling grid in a space where the ceiling is a pressure boundary. High-bay fixtures hang forty feet above equipment that cannot be moved, in a room where a lift cannot be staged. The result is that routine service becomes a project, and a project gets deferred.
- The sealing system does not match the cleaning chemistry. IP66 and NEMA 4X describe resistance to ingress; they do not describe resistance to a quaternary ammonium compound, a peracetic acid fogging cycle, or a caustic washdown at 140 °F applied three times a day. Gasket compound, lens material, fastener alloy, and finish system all matter. Fixtures selected on rating alone frequently pass the paperwork and fail in service, and a compromised seal in a controlled space is both a maintenance event and a contamination question. This is the practical difference between harsh-environment and hazardous-location specification, and the two are not interchangeable.
- Thermal design was treated as a datasheet footnote. In LED systems, the driver usually fails before the diodes do, and heat is the reason. A luminaire rated to 40 °C ambient that is actually installed at 55 °C — above a dryer, near an oven, in a poorly circulated ceiling plenum — will not deliver its published life. LM-80 test data and TM-21 projections are only meaningful when the operating ambient in the specification matches the operating ambient in the room. Thermal headroom is the cheapest maintenance-risk reduction available at design time.
- Documentation and configuration control were left to the submittal package. Five years after commissioning, the question is not “what did we buy?” but “can we get the same thing again?” If the SKU has been discontinued, if the replacement has a different photometric distribution or a different mounting footprint, or if the fixture was modified in the field without records, the replacement becomes a change control exercise rather than a stores transaction.
- Emergency and egress lighting was scoped separately. In classified areas, egress fixtures carry their own listings and their own testing obligations. When they are procured outside the main lighting package, they tend to be the fixtures nobody has spare parts for.
Designing the Risk Out
The good news is that each of these is addressable at specification time, and none of them require exotic products.
Specify the service plan alongside the fixture. Before selecting a luminaire, decide who services it, from where, how often, and what has to be shut down to allow it. Surface-mounted or pendant fixtures serviceable from below are often preferable to recessed units in spaces where the ceiling is a barrier. Remote-driver configurations move the most failure-prone component out of the controlled space entirely — sometimes the single highest-leverage decision on a project.
Select for the cleaning protocol, not the room name. Ask for the actual chemistry, concentration, temperature, and frequency, then confirm material compatibility for gaskets, lenses, and hardware. Stainless fasteners, fluorosilicone or silicone gasketing, tempered glass, and appropriate finish systems cost more up front and considerably less over a decade.
Build in thermal and lumen margin. Specify to the true worst-case ambient. Target the required maintained illuminance at end of life, not out of the box, so that lumen depreciation does not force an early intervention. DesignLights Consortium listings and IES recommended practices are useful reference points, but the governing number is the maintained level your qualification documents require.
Treat documentation as a deliverable. Spec sheets, photometric files, listing documentation, and BIM/Revit families should be part of the handover — and the replacement-part path should be understood before purchase, not after a failure. Working with a manufacturer that maintains configuration records for custom or modified fixtures is materially different from buying a catalog item from a distributor who may not stock it in three years.
Never modify a listed fixture informally. In a classified area, mounting changes, gland substitutions, and bracket fabrication all interact with the listing. These changes can often be made — but they have to be engineered and documented, not improvised.
The Catalog Trap
The recurring failure mode in controlled-environment lighting is selection by specification sheet comparison: matching wattage, lumens, CCT, and price across three manufacturers and choosing the lowest number. Those four values say nothing about serviceability, chemical compatibility, thermal margin, listing scope, or long-term parts availability — which is to say, they say nothing about maintenance risk.
A better approach treats lighting in a cleanroom, aseptic suite, or classified process area as an application-specific system: defined by the room’s classification, its cleaning regime, its thermal profile, its access constraints, its qualification requirements, and the documentation the owner will need to live with. SpecGrade’s hazardous location and specification-grade product lines are built around that premise, and our education resources cover the Class/Division framework in more detail for teams working through classification questions.
If you are scoping a controlled-environment lighting package and want a second set of eyes on serviceability and compliance before the specification is locked, contact our engineering team or find your local representative.
About The Author
This article was written by Rick Nathans, CEO, and Doug Lauck, COO, of SpecGrade, a Columbus, Ohio manufacturer of commercial and industrial LED lighting since 2010.
SpecGrade is currently involved in multiple projects that are subject to non-disclosure agreements. While project names and customer details cannot be shared, the team can share the application and engineering lessons that arise during complex lighting evaluations.
One example involved modifying the mounting brackets for a specified hazardous-location luminaire while maintaining UL 844 compliance. To support the project’s engineering team, SpecGrade also developed the required BIM/Revit documentation for the modified fixture configuration. This type of coordination illustrates why cleanroom and controlled-environment lighting should be evaluated as an application-specific system—not simply selected from a catalog based on wattage or lumen output.