When Pharmaceutical Manufacturing Lighting Requires Hazardous-Location Protection
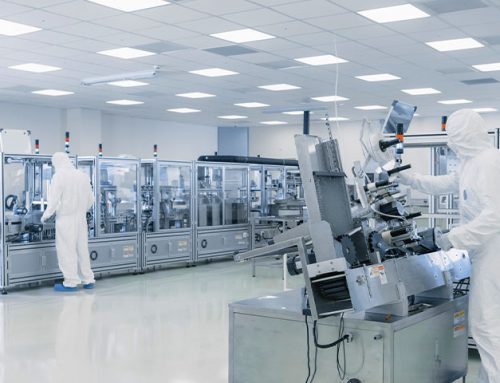
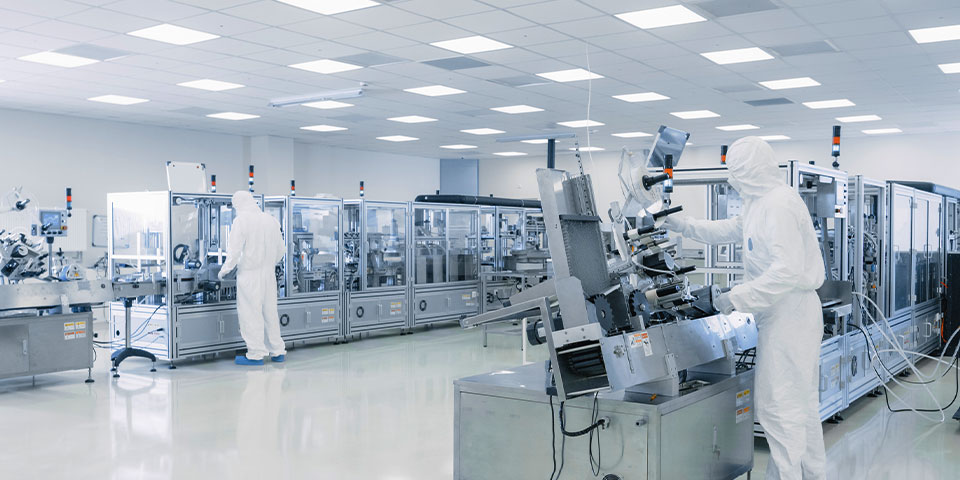
Most of a pharmaceutical facility is not a hazardous location. Filling suites, packaging halls, warehouses, QC labs, and the majority of oral solid dose areas are unclassified spaces where the governing lighting concerns are cleanability, illuminance, and glare. Then there are the rooms where that changes — and where installing an ordinary luminaire is not merely a suboptimal choice but a code violation with real ignition risk behind it.
The difficulty is that the boundary between those two categories is not obvious from a floor plan, and it is frequently drawn wrong in both directions. Some projects over-specify, putting heavy cast explosion-proof fixtures in rooms that were never classified — paying twice the cost and inheriting a fixture that is difficult to clean in a GMP space. Others under-specify, discovering at inspection that the solvent dispensing booth in the corner of an otherwise ordinary room brought a classification with it.
This article covers where hazardous-location lighting is actually required in pharmaceutical manufacturing, how that determination gets made, and what makes pharmaceutical classified areas harder to specify for than the refineries and chemical plants these products were originally designed around.
The Classification Comes First — and It Is Not the Lighting Designer’s Call
Under the National Electrical Code, an area is classified through a documented engineering determination, not an assumption. NFPA 70 Article 500 requires that classified areas be documented and that the documentation be available to those responsible for design, installation, inspection, and maintenance. The underlying analysis usually follows NFPA 497 for flammable gases and vapors and NFPA 499 for combustible dusts, with combustible-dust requirements now consolidated into NFPA 660 — confirm which edition your authority having jurisdiction enforces. OSHA’s hazardous location requirements then require that equipment installed in those areas be approved for the class, division, and group involved.
Practically, this means the first question in any pharmaceutical lighting scope is not “what fixture should we use?” but “where is the area classification drawing, who sealed it, and when was it last revised?” If nobody can produce it, the lighting package is not ready to specify. Classification drawings age badly — process changes, solvent substitutions, and ventilation modifications all shift boundaries, and the lighting installed under a 2011 drawing may not comply with the 2024 revision.
Where Pharmaceutical Classification Typically Applies
Across API synthesis, oral solid dose, sterile injectable, and inhalation manufacturing, the classified areas tend to cluster in a predictable set of operations:
Solvent storage, dispensing, and charging. Flammable liquid storage rooms, weigh-and-dispense booths, and reactor charging stations handling ethanol, isopropyl alcohol, acetone, methanol, heptane, or toluene are the most common classified spaces in pharmaceutical plants. Quantity, container handling method, and ventilation drive whether the result is Division 1, Division 2, or unclassified.
Wet granulation and solvent-based coating. Fluid bed processors and pan coaters running organic solvent systems create classified envelopes around the equipment, exhaust, and solvent supply — even when the surrounding room is not classified.
Solvent recovery and distillation. Recovery skids, condensers, and waste solvent handling are frequently classified, and are often located in utility spaces where the lighting scope gets less scrutiny than it does in the suites.
Combustible dust operations. Milling, sieving, blending, tablet compression, and dust collection can generate ignitable concentrations of pharmaceutical powders. Lactose, starch, and microcrystalline cellulose are combustible, and OSHA treats combustible dust as a recognized hazard in pharmaceutical manufacturing. Where the analysis finds an ignitable dust cloud or a hazardous layer accumulation, Class II classification follows.
Specialty operations. Hydrogenation with hydrogen supply, metered-dose inhaler filling with liquefied propellant, ethylene oxide sterilization, and gas cylinder rooms each bring their own classification, and several of them fall outside the Group D materials most catalog fixtures are listed for.
Class, Division, and Group — the Three Values That Drive Fixture Selection
A hazardous-location listing is not a single quality rating; it is a specific scope, and a fixture that is listed for the wrong scope is no better than an unlisted one.
Class identifies the hazard type: flammable gases and vapors (Class I), combustible dust (Class II), or ignitable fibers and flyings (Class III). Division identifies likelihood: present under normal operation (Division 1), or only under abnormal conditions such as a spill, leak, or ventilation failure (Division 2). Group identifies the specific material family. Most pharmaceutical solvents fall in Group D, but hydrogen service is Group B, and pharmaceutical dusts are typically Group G.
The distinction that costs the most money is Division 1 versus Division 2. Division 1 generally requires explosion-proof construction — flamepaths, pressure-containing housings, sealed conduit entries. Division 2 permits a broader and considerably less expensive range of designs. A great many products marketed loosely as “explosion proof” carry Division 2 listings only, so the UL 844 marking on the nameplate — not the marketing copy — is what governs. Our Class/Division education resource walks through the framework in more detail.
Temperature code deserves its own check. In Class I areas, the fixture’s T-code must stay below the autoignition temperature of the material present. Most common pharmaceutical solvents have autoignition temperatures comfortably above a T4 (135 °C) rating, but low-AIT materials such as diethyl ether do not leave much margin — which makes the T-code an actual calculation rather than a box to tick. In Class II areas the logic changes entirely: the governing limits derive from dust layer and cloud ignition temperatures with a code-mandated safety margin, so a Class I T-code does not transfer across.
What Makes Pharmaceutical Classified Areas Harder Than Refineries
Hazardous-location luminaires were engineered for oil and gas. Those environments are demanding, but they do not ask the fixture to be cleanable to GMP standards. Pharmaceutical classified areas ask for both at once, and the two requirement sets pull against each other.
Explosion-proof construction favors heavy cast aluminum housings with cooling fins, external fasteners, and threaded entries — geometry that traps particulate and resists effective cleaning. GMP construction favors smooth, crevice-free, flush surfaces that can be wiped down and will tolerate repeated exposure to sporicidal agents. A fixture that satisfies one specification often fails the other.
The practical resolutions are usually geometric rather than material: keeping the luminaire outside the classified envelope where the classification permits it; using remote-driver configurations to move components out of the controlled space; selecting linear hazardous-location luminaires with cleaner profiles and stainless hardware rather than traditional high-bay castings; and confirming that gasketing and finish systems tolerate the actual cleaning chemistry rather than just the ingress rating. That last point is where harsh-environment and hazardous-location requirements diverge, and conflating them is a common source of premature failure.
Egress lighting is the piece most often missed. A classified area still needs emergency illumination and exit marking, and those fixtures need both a hazardous-location listing and UL 924 for emergency operation — as on a dual-listed exit sign. When egress is procured separately from the main lighting package, it tends to be the scope where compliance gaps appear.
A Short Decision Sequence
Before specifying anything for a pharmaceutical area that might be classified, work through five questions in order: Is there a current, sealed area classification drawing? What class, division, and group apply at the specific fixture location, not the room as a whole? Does the classification depend on ventilation that could fail or be interlocked out? What cleaning protocol and GMP surface requirements apply on top of the hazardous-location listing? And are emergency, egress, and controls in the same space covered by the same analysis?
Answer those and the fixture selection becomes straightforward. Skip them and the specification is a guess — one that will be audited. If you are working through classification boundaries on a pharmaceutical project, our hazardous location and specification-grade teams are available to review scope before the package is locked. Contact our engineering group or reach your local representative.
About The Author
This article was written by Rick Nathans, CEO, and Doug Lauck, COO, of SpecGrade, a Columbus, Ohio manufacturer of commercial and industrial LED lighting since 2010.
SpecGrade is currently involved in multiple projects that are subject to non-disclosure agreements. While project names and customer details cannot be shared, the team can share the application and engineering lessons that arise during complex lighting evaluations.
One example involved modifying the mounting brackets for a specified hazardous-location luminaire while maintaining UL 844 compliance. To support the project’s engineering team, SpecGrade also developed the required BIM/Revit documentation for the modified fixture configuration. This type of coordination illustrates why cleanroom and controlled-environment lighting should be evaluated as an application-specific system—not simply selected from a catalog based on wattage or lumen output.